Dimensional Inspection Before vs After Machining: Why Both Matter
In modern manufacturing, dimensional inspection is not limited to checking the finished component. Quality can be controlled at different stages of production, from the initial raw material, casting, or forging through machining and final inspection.
Two important stages are:
Dimensional Inspection Before Machining and Dimensional Inspection After Machining.
Although both involve measurement, they serve different purposes.
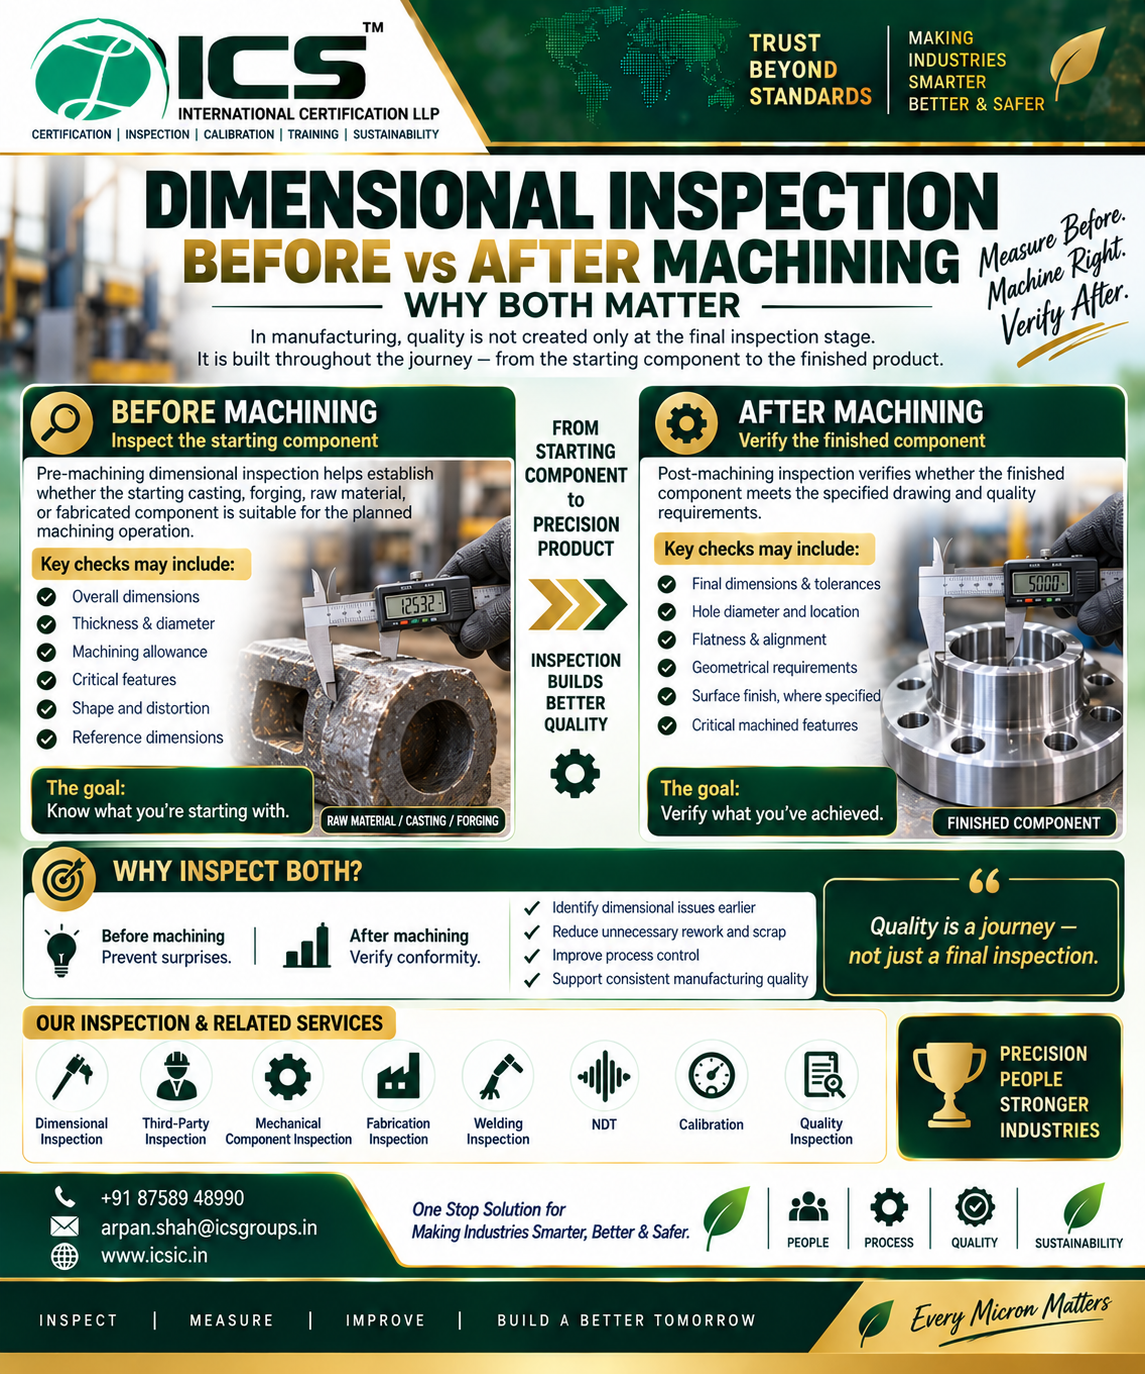
Inspect Before. Machine Right. Verify After.
This approach can help manufacturers identify dimensional issues early, reduce unnecessary rework, improve process control, and increase confidence in the final product.
What Is Dimensional Inspection?
Dimensional inspection is the process of measuring a component’s physical dimensions and comparing them with specified requirements.
Depending on the component and engineering drawing, dimensional inspection may include:
- Length and width
- Height and thickness
- Diameter
- Hole diameter
- Hole location
- Centre-to-centre distance
- Flatness
- Straightness
- Parallelism
- Perpendicularity
- Alignment
- Runout
- Other specified dimensional or geometrical characteristics
The inspection requirements should always be based on the applicable engineering drawing, specification, standard, purchase order, or customer requirement.
Dimensional Inspection Before Machining
Before machining begins, dimensional inspection helps determine the starting condition of the component.
This can apply to:
- Castings
- Forgings
- Raw material
- Plates
- Bars
- Welded components
- Fabricated structures
- Semi-finished components
The objective is to confirm whether the starting component is suitable for the next manufacturing operation.
Common Pre-Machining Checks
Depending on the component, inspectors may verify:
📏 Overall Dimensions
Length, width, height, thickness, diameter, or other relevant dimensions may be checked.
⚙️ Machining Allowance
The available material must be sufficient to achieve the required final dimensions.
If the starting component is undersized, machining may not be able to produce the required final dimension.
🔍 Critical Features
Important locations, reference surfaces, holes, or other features may need to be verified before machining.
📐 Distortion and Shape
Castings, forgings, and fabricated components can have dimensional variations or distortion that may affect machining.
Why Is Inspection Before Machining Important?
Consider a forged component that needs to be machined to a specific final diameter.
If the starting diameter is already too small, there may not be enough material available to achieve the required final dimension.
If this is discovered before machining, the component can be identified and evaluated before significant machining time and resources are invested.
This gives manufacturers an important quality-control advantage:
Find the problem before adding more value to the component.
Pre-machining inspection can therefore help prevent unsuitable components from unnecessarily progressing through production.
Dimensional Inspection After Machining
Once machining is complete, dimensional inspection verifies the finished component against the specified requirements.
The objective is to determine whether the machining process has produced the required result.
Depending on the drawing and component, post-machining inspection may include:
- Final dimensions
- Dimensional tolerances
- Hole diameters
- Hole locations
- Centre distances
- Flatness
- Parallelism
- Perpendicularity
- Runout
- Alignment
- Surface finish, where specified
- Other critical characteristics
The final inspection results can then be evaluated against the applicable acceptance criteria.
Why Is Post-Machining Inspection Important?
Machining accuracy can be affected by several factors, including:
- Tool wear
- Machine condition
- Incorrect setup
- Fixture problems
- Programming errors
- Incorrect cutting parameters
- Thermal effects
- Operator technique
- Material movement
As a result, even when the starting component is correct, the final machined component may not necessarily meet every specified requirement.
Post-machining inspection provides an opportunity to verify the actual finished condition.
The key question is:
“Does the finished component meet the drawing requirements?”
Before vs After Machining: What Is the Difference?
The easiest way to understand the two inspection stages is to look at their objectives.
BEFORE MACHINING
Purpose: Check the starting condition.
It helps answer:
“Is the component suitable for machining?”
AFTER MACHINING
Purpose: Verify the finished condition.
It helps answer:
“Has machining produced the required result?”
Therefore:
Before machining = Verify what you have.
After machining = Verify what you achieved.
Why Both Inspections Can Be Valuable
Inspecting only the finished component provides information about the final result, but it may not tell you what the starting condition was.
When inspection is performed at appropriate stages, manufacturers can obtain greater visibility into the manufacturing process.
A typical flow can be:
Raw Material / Casting / Forging
↓
Pre-Machining Dimensional Inspection
↓
Machining
↓
Post-Machining Dimensional Inspection
↓
Final Inspection
This approach can help identify where dimensional variation is introduced.
Example: Machined Shaft
Imagine a shaft that must meet a specified final diameter.
Before Machining
The starting shaft is inspected to confirm that the available material and relevant dimensions are suitable for machining.
During Machining
The component is machined according to the applicable manufacturing process and requirements.
After Machining
The finished diameter is measured using a suitable measuring instrument.
The result is compared with the specified tolerance.
If the dimension is within the applicable acceptance criteria, the characteristic can be accepted.
If it is outside the requirement, the component may require further evaluation, rework, or other disposition according to the applicable quality procedure.
This example demonstrates how inspection before and after machining provides different information.
Example: Fabricated Component
Dimensional inspection can also be important when fabricated components are subsequently machined.
Fabrication processes, especially welding, can introduce dimensional changes due to:
- Heat input
- Welding distortion
- Material movement
- Fit-up variation
- Clamping conditions
A dimensional check before machining can establish the actual condition of the fabricated component.
After machining, another inspection can verify the final dimensions.
This creates a stronger connection between fabrication quality, machining quality, and final product quality.
Measuring Instruments Used for Dimensional Inspection
Different components require different measuring instruments.
The instrument should be selected based on the characteristic being measured, tolerance, required resolution, and intended application.
📏 Vernier Caliper
Commonly used for general dimensional measurements such as external dimensions, internal dimensions, and depths within its capability.
🔧 Micrometer
Suitable for many precision external dimensional measurements where its range and resolution meet the requirement.
📐 Height Gauge
Used for suitable height and feature-location measurements from a reference surface.
🔍 Bore Gauge
Used for measuring suitable internal diameters.
⚙️ Dial Indicator
Useful for comparative measurements such as runout, alignment, and variation.
🖥️ Coordinate Measuring Machine (CMM)
CMMs can measure multiple dimensional and geometrical characteristics of suitable components.
🔬 Specialized Gauges
Depending on the application, thread gauges, plug gauges, ring gauges, profile gauges, and other specialized equipment may be used.
The key principle is:
Use the right instrument for the right measurement.
Calibration: A Critical Part of Dimensional Inspection
Reliable dimensional inspection depends on appropriately controlled measuring equipment.
Measuring instruments should be managed according to the organization’s measurement-control system and applicable requirements.
This can include:
- Equipment identification
- Calibration status
- Calibration records
- Defined calibration intervals
- Equipment maintenance
- Proper storage
- Protection from damage
- Suitability checks before use
Calibration provides evidence that an instrument’s measurement performance has been evaluated against appropriate standards under defined conditions.
However, calibration alone does not guarantee a reliable measurement.
Measurement reliability also depends on:
Instrument + Method + Conditions + Operator + Measurement Requirement
Common Dimensional Inspection Problems
Several issues can affect dimensional inspection results.
❌ Wrong Instrument Selection
An instrument may not have suitable accuracy, resolution, or range for the required tolerance.
❌ Incorrect Measurement Method
Improper positioning or measurement technique can affect the result.
❌ Poor Alignment
Incorrect alignment between the instrument and component feature can introduce measurement errors.
❌ Dirty Components
Chips, oil, dirt, or other contamination can affect measurements.
❌ Temperature Effects
Component and instrument temperatures can influence precision measurements.
❌ Tool Wear
Machining tool wear can gradually affect final dimensions.
❌ Incorrect Datum or Reference
Using an incorrect reference surface can lead to incorrect dimensional evaluation.
❌ Incorrect Recording
Even a correct measurement can create a quality problem if it is recorded against the wrong characteristic or component.
The Cost of Skipping Pre-Machining Inspection
A dimensional problem discovered early can often be easier to manage than one discovered after several manufacturing operations.
Imagine a component that has:
Casting → Heat Treatment → Machining → Surface Treatment → Assembly
If an unsuitable starting dimension is not identified until final inspection, the organization may have already invested considerable time and resources.
Potential consequences can include:
- Rework
- Scrap
- Additional machining
- Production delays
- Material wastage
- Additional inspection
- Delivery delays
- Customer rejection
This is why inspection timing matters.
Does Every Component Need Inspection Before and After Machining?
Not necessarily.
The inspection strategy should be based on factors such as:
- Component criticality
- Drawing requirements
- Tolerances
- Manufacturing process
- Customer requirements
- Risk
- Inspection and Test Plan
- Quality procedures
- Applicable standards
- Previous process performance
The objective is not to perform unnecessary inspection.
The objective is to establish appropriate inspection points that provide effective control of product quality.
Dimensional Inspection and Quality Control
Dimensional inspection is an important part of quality control, but it should not be viewed as an isolated activity.
An effective manufacturing quality system connects:
Requirement
↓
Material / Component Verification
↓
Process Control
↓
Dimensional Inspection
↓
Corrective Action Where Required
↓
Final Verification
↓
Conforming Product
This process-oriented approach can help organizations move from simply finding problems toward preventing problems.
Dimensional Inspection in Third-Party Inspection
Third-Party Inspection (TPI) can include dimensional inspection depending on the agreed inspection scope.
For manufactured, fabricated, cast, forged, or machined components, inspection activities may include:
- Drawing review
- Material verification
- Dimensional inspection
- Visual inspection
- Welding inspection
- NDT
- Surface finish inspection
- Documentation review
- Final inspection
- Pre-dispatch inspection
Independent inspection can provide customers and other stakeholders with additional confidence that specified requirements have been verified.
The exact inspection scope and acceptance criteria should be defined by the applicable project documentation and contractual requirements.
How Manufacturers Can Improve Dimensional Quality
Organizations can strengthen dimensional quality by:
✅ Identifying critical dimensions
✅ Performing inspection at appropriate manufacturing stages
✅ Selecting suitable measuring instruments
✅ Maintaining calibration controls
✅ Using standardized measurement methods
✅ Training inspection personnel
✅ Monitoring machining processes
✅ Controlling reference surfaces and datums
✅ Maintaining traceable inspection records
✅ Investigating recurring dimensional deviations
The goal is not simply to measure more.
The goal is to measure smarter.
A Simple Quality Philosophy
The concept can be summarized in three steps:
1. Inspect Before
Understand the starting condition and confirm suitability for the next operation.
2. Machine Right
Control the machining process using the correct process parameters, equipment, tools, and procedures.
3. Verify After
Confirm that the finished component meets the applicable requirements.
Therefore:
Inspect Before. Machine Right. Verify After.
Final Takeaway
Dimensional Inspection Before vs After Machining is not simply a comparison between two inspection activities.
It represents two different opportunities to control quality.
Before machining, inspection helps identify whether the starting component is suitable and whether sufficient material and relevant dimensions are available for machining.
After machining, inspection verifies whether the finished component meets its specified dimensional and geometrical requirements.
When used appropriately, inspection at both stages can help manufacturers:
✔️ Detect problems earlier
✔️ Reduce unnecessary rework
✔️ Control manufacturing processes
✔️ Improve dimensional accuracy
✔️ Reduce scrap
✔️ Strengthen quality assurance
✔️ Improve customer confidence
Quality is not created only at the final inspection. It is built throughout the manufacturing journey.
Measure Before. Machine Right. Verify After.
About ICS International Certification LLP
ICS International Certification LLP provides professional inspection, calibration, certification, training, and quality services to industries.
Our services include:
🔹 Dimensional Inspection
🔹 Third-Party Inspection
🔹 Mechanical Component Inspection
🔹 Fabrication Inspection
🔹 Welding Inspection
🔹 Visual Inspection
🔹 NDT Inspection
🔹 Surface Finish Inspection
🔹 Calibration Services
🔹 Quality Inspection
🔹 Management System Certification
🔹 Training & Competency Development
One Stop Solution for Making Industries Smarter, Better & Safer.
📞 +91 87589 48990
📧 arpan.shah@icsgroups.in
🌐 www.icsic.in